Where the part goes
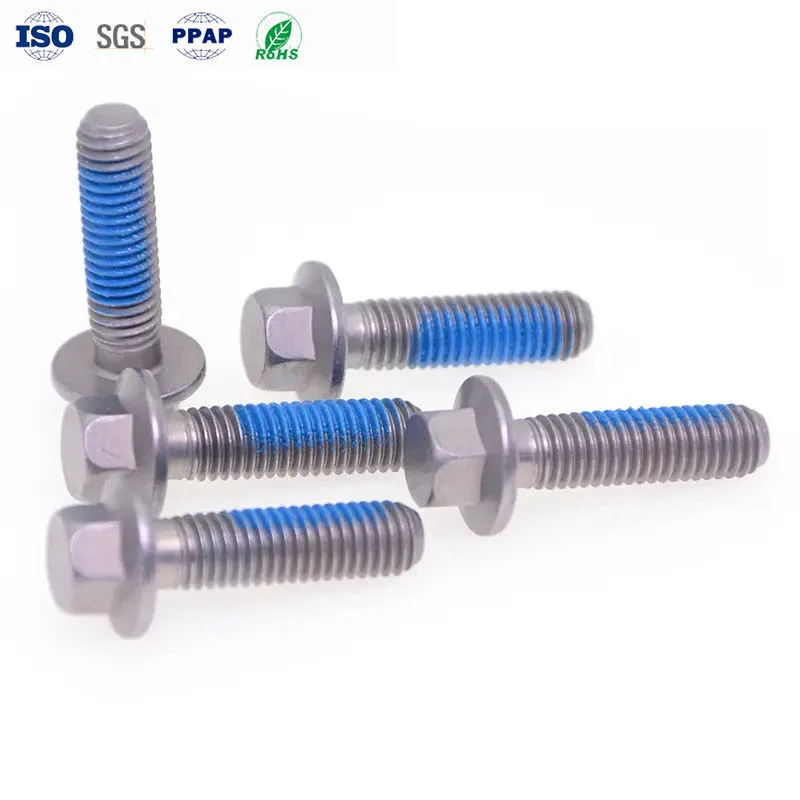
Chassis brackets, subframe mounts and underbody assemblies — joints that are torqued once at the plant and then spend fifteen years being rained on. The flange under the head spreads clamp load over a wider footprint than a plain hex head, so the joint can use a shorter bolt and skip the separate washer, which is one less part on the line and one less thing to drop.
What it has to survive
Road salt first. The zinc-nickel layer on this bolt holds 720 hours of neutral salt spray before red rust — well past what a plain zinc electroplate manages, and without the coating build-up that would jam a thread. Where a customer needs more, we quote the finish and the tested hours together rather than promising a number in isolation.
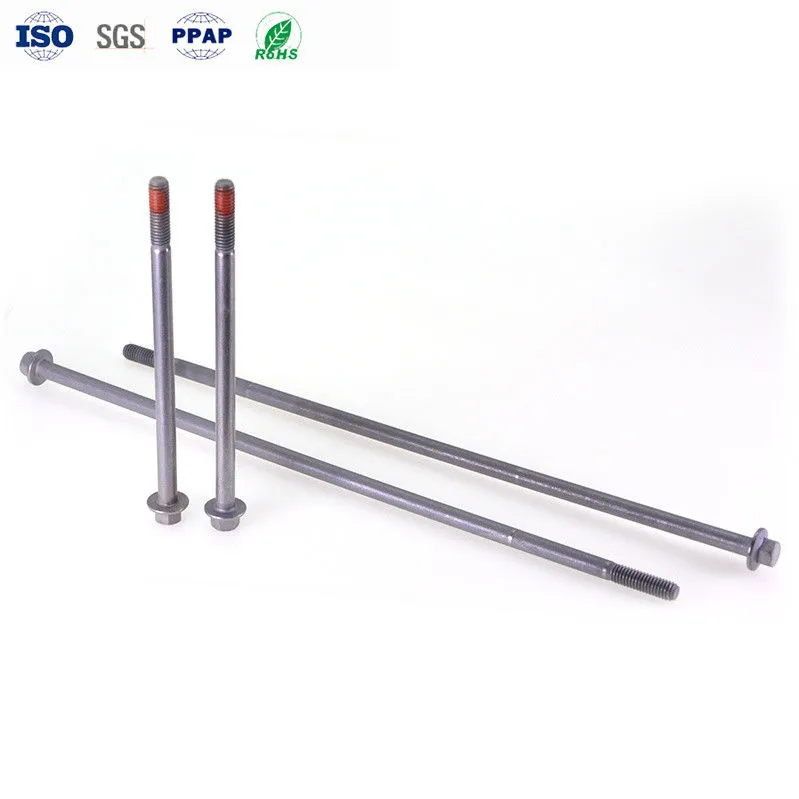
Vibration second. Every bolt ships with a pre-applied Nylok patch on the thread, so prevailing torque comes from the fastener instead of a threadlocker dispensed on the line — no curing time, no contamination of the joint face, and a re-use behaviour the assembly station can plan around.
How it is made
Cold heading, thread rolling, heat treatment, then plating. Forming and threading happen in our workshop; heat treatment and plating run through qualified partners we audit every year, and the property class on the box is the class we tested, not the class we aimed for.
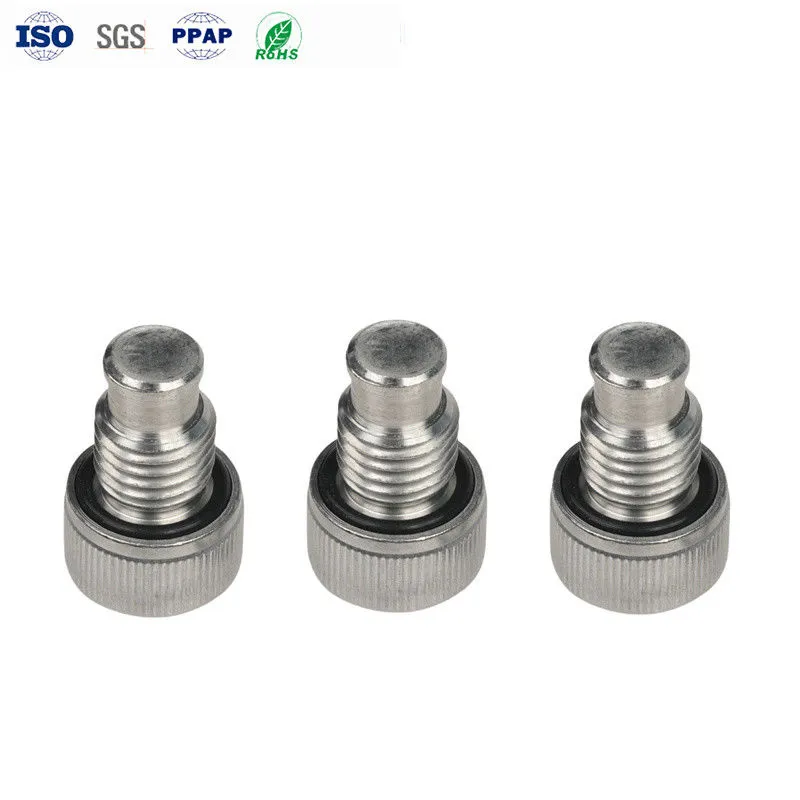
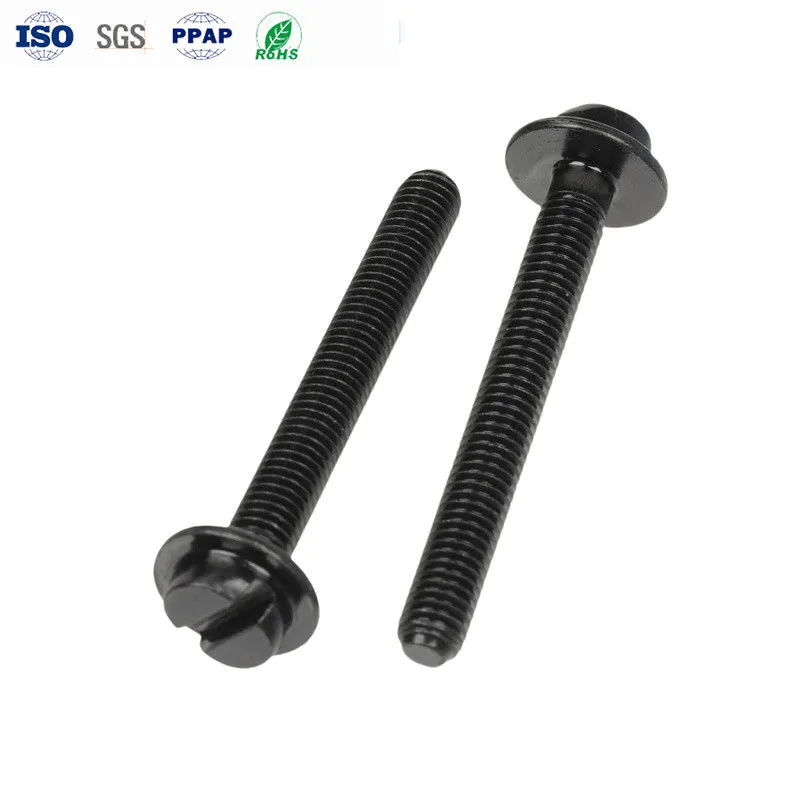
Range: M2.0 to M16, 4 mm to 400 mm long, metric or inch threads, to DIN, ISO, ANSI or GB. Head and drive geometry is open — flange, hex, pan, socket — because the tooling is ours.
How we prove it
Hardness, breaking torque, tensile strength and dimensional checks run in our own lab, and the performance report travels with the lot instead of being emailed on request. Thread gauges are checked at the start and end of each run. RoHS documentation and a third-party SGS environmental report come with the shipment, and FAI or PPAP packages are available when the customer’s quality system asks for them.
Where the limits are
Minimum order is 1,000 pieces, and free samples are available before that. Lead time runs 10 days to 10,000 pieces, 15 days to 50,000, 20 days to 100,000, and is quoted per schedule above that. A property class above 12.9, or a head geometry that needs new tooling, starts with a drawing review — we would rather quote the tooling up front than discover it in the first lot.
Numbers
| Attribute | Detail |
|---|---|
| Material | SCM435 alloy steel |
| Property class | 8.8 / 10.9 / 12.9 |
| Thread | M2.0–M16, metric or inch, to DIN / ISO / ANSI / GB |
| Length | 4–400 mm |
| Finish | Zinc-nickel alloy |
| Corrosion | 720 h neutral salt spray |
| Locking | Pre-applied Nylok patch |
| Testing | Hardness, breaking torque, tensile strength, dimensional — in-house lab |
| Certification | ISO 9001 / IATF 16949 / ISO 14001 / RoHS, SGS report |
| MOQ | 1,000 pcs |
| Lead time | 10 / 15 / 20 days at 10K / 50K / 100K pcs |